

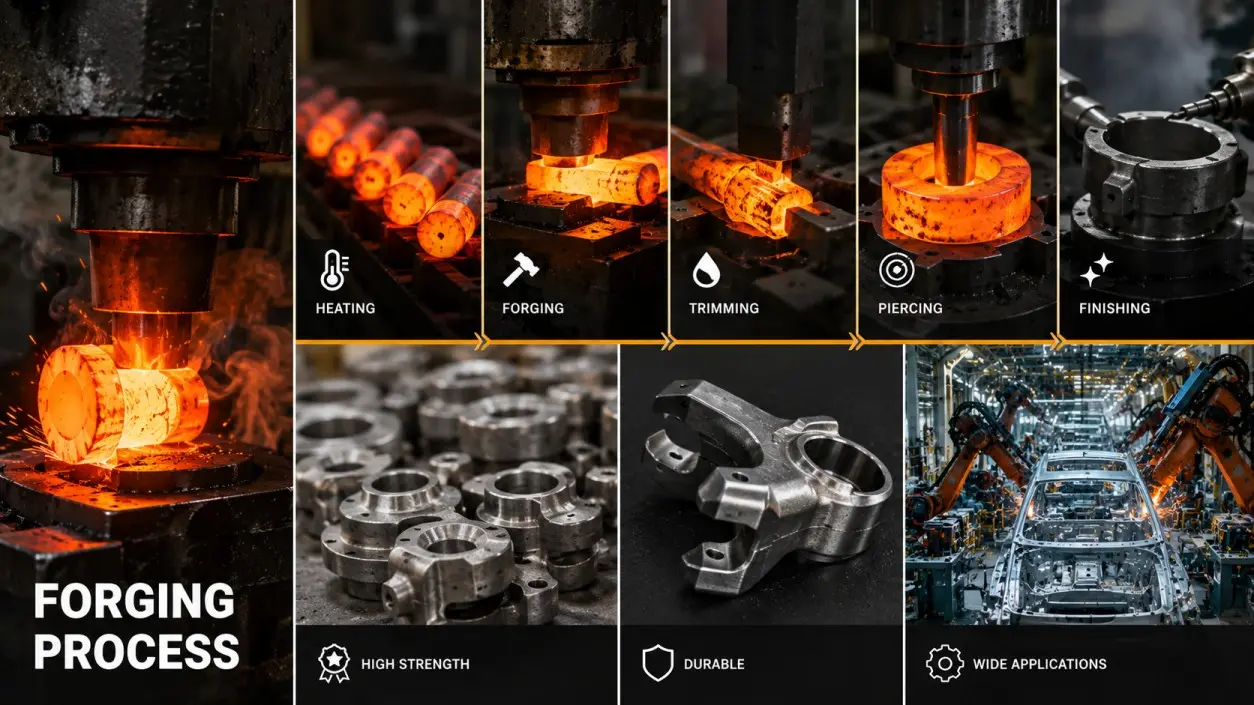
Forging Process Explained: Types, Steps, Advantages & Industrial Applications
The forging process is one of the oldest and most reliable methods of shaping metal for industrial use. It works by applying controlled compressive force to a heated or cold metal workpiece — using hammering, pressing, or rolling — to reshape the metal into a stronger, denser, and more dimensionally accurate component than what casting, machining, or fabrication alone can achieve.
What makes forging different from other metalworking processes is what happens inside the metal during deformation. When a billet is forged, its internal grain structure realigns to follow the contour of the finished part. This grain flow refinement eliminates internal voids, closes porosity, and distributes material density evenly across the cross-section. The result is a component with superior mechanical strength, fatigue resistance, and impact toughness compared to a cast or machined equivalent of the same material grade.
For engineers, procurement managers, OEM buyers, and plant owners evaluating manufacturing methods for critical components, understanding how the forging process works — and where it outperforms alternatives — is essential for making the right specification and sourcing decisions.
What Is the Forging Process?
The forging process is a solid-state metal forming operation in which a metal workpiece — typically a billet, bar, or ingot — is heated to a temperature where the metal becomes plastically deformable (in hot forging) or is deformed at room temperature (in cold forging), and then shaped using compressive force applied through dies, hammers, or presses.
Unlike casting, where molten metal is poured into a mold and solidifies into shape, forging reshapes metal in its solid state. No melting occurs. The metal is squeezed, pressed, or hammered between dies that define the final geometry. This solid-state deformation is what gives forged components their characteristic strength — the metal’s grain structure is physically refined and oriented by the forming force, creating a continuous grain flow that follows the shape of the part.
The forging process has been used for thousands of years — from blacksmiths forging blades and horseshoes to modern hydraulic presses producing aerospace turbine discs and automotive crankshafts. The core principle has never changed: compressive force applied to solid metal produces stronger components than any other forming method.
Types of Forging Processes
Forging processes are classified by two criteria — the temperature at which the metal is deformed and the type of die or tooling used to shape it.
Classification by Temperature
Temperature is usually the first decision rather than the last. We have looked at hot forging and cold forging compared side by side, including where closed die work sits between them.
Hot Forging
Hot forging is performed at temperatures above the metal’s recrystallization point — typically between 950°C and 1,250°C for carbon and alloy steels. At these temperatures, the metal’s yield strength drops significantly, allowing it to be deformed with less force and shaped into complex geometries with minimal risk of cracking.
Hot forging is the most common forging method for industrial components. It is used to produce crankshafts, connecting rods, gear blanks, flanges, valve bodies, and structural parts in carbon steel, alloy steel, and stainless steel.
The main advantages of hot forging are lower forming force requirements, better material flow into complex die cavities, and the ability to forge large cross-sections. The main limitations are surface oxidation (scale formation), tighter dimensional tolerances are harder to hold, and post-forging machining is usually required to reach final dimensions.
Warm Forging
Warm forging is performed at temperatures between 200°C and 850°C — below the recrystallization temperature but above room temperature. This range offers a balance between the formability of hot forging and the dimensional accuracy of cold forging.
Warm forging is used for medium-complexity components where tighter tolerances than hot forging are needed but full cold forging force is impractical. Common warm-forged products include automotive transmission components, bearing races, and precision gear blanks.
Cold Forging
Cold forging is performed at room temperature. The metal workpiece is deformed without any heating, which means the finished component retains excellent surface finish, tight dimensional tolerances, and work-hardened strength without additional heat treatment.
Cold forging is used for high-volume production of smaller components such as bolts, nuts, screws, pins, rivets, ball studs, and small precision parts. The main advantage is near-net-shape accuracy — many cold-forged parts require zero or minimal post-forging machining. The main limitation is that the forming force required is significantly higher than hot forging, which restricts cold forging to smaller components and more ductile materials.
Classification by Die Type
Open Die Forging
In open die forging, the workpiece is placed between two flat or simply shaped dies that do not fully enclose the metal. The dies compress the workpiece from above and below while the metal is free to flow laterally. The operator or machine repositions and rotates the workpiece between successive hammer or press strokes to build up the desired shape progressively.
Open die forging is used for large, heavy components — shafts, cylinders, discs, sleeves, rings, and blocks — typically in sizes and weights that exceed the capacity of closed die forging equipment. Components weighing several hundred kilograms to several tonnes are routinely produced by open die forging.
The advantages of open die forging are the ability to produce very large parts, flexibility to accommodate custom shapes without expensive dedicated dies, and excellent internal grain structure refinement. The limitation is that dimensional accuracy is lower than closed die forging, so more post-forging machining is typically required.
Closed Die Forging (Impression Die Forging)
In closed die forging, the workpiece is placed between two shaped dies that contain the full impression of the desired part. When the dies close under high force — delivered by a mechanical press, hydraulic press, or drop hammer — the metal fills the die cavity and takes the shape of the impression. Excess material is squeezed out as flash, which is trimmed after forging.
Closed die forging produces components with tighter dimensional tolerances, better surface finish, and higher production consistency than open die forging. It is the standard method for medium-volume and high-volume production of automotive parts, aerospace components, oil and gas fittings, hand tools, and industrial hardware.
The main advantage is repeatability — every part produced from the same die set is dimensionally identical. The main limitation is the cost of die tooling, which makes closed die forging uneconomical for very low quantities or very large components.
Roll Forging
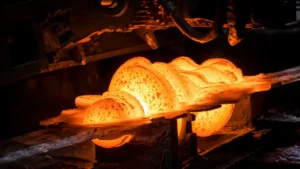
Roll forging passes a heated bar or billet between two rotating cylindrical dies that progressively reduce its cross-section and increase its length. The process produces elongated components with uniform cross-sections — shafts, axles, leaf springs, and tapered blanks.
Roll forging is continuous and fast, making it efficient for high-volume production of symmetrical elongated parts.
Upset Forging
Upset forging increases the diameter of a workpiece by compressing its length. A heated bar is held in a stationary die while a punch or ram compresses one end, causing the metal to “upset” — or bulge — into a larger diameter head or flange.
Upset forging is the standard method for producing bolt heads, fastener heads, valve stems, and similar components where a localized increase in cross-section is needed at one end of an elongated part.
Ring Rolling
Ring rolling produces seamless rings from a hollow preform. The preform is placed between two rolls — an inner mandrel and an outer drive roll — that simultaneously compress the ring wall while expanding its diameter. The result is a seamless ring with circumferential grain flow and excellent mechanical properties.
Ring rolling is used for bearing races, flanges, gear rings, turbine casings, and large structural rings for wind turbines and aerospace applications.
Forging Process Steps
While the specific steps vary by forging method and component complexity, the general forging process follows a consistent sequence.
Step 1 — Material Selection
The process begins with selecting the correct material grade for the application. The choice of base metal — carbon steel, alloy steel, stainless steel, aluminum, titanium, or copper alloy — determines the forging temperature, forming force, die design, and post-forging heat treatment requirements.
Material is typically sourced as billets, bars, or ingots with certified chemical composition and mechanical properties documented in a mill test certificate.
Step 2 — Billet Cutting and Preparation
The raw material is cut to the required billet weight and dimensions. Accurate billet weight is critical in closed die forging — too little material results in underfill (incomplete die filling), and too much material produces excessive flash and wastes material.
The billet surface is inspected for cracks, seams, and scale before proceeding to heating.
Step 3 — Heating
For hot forging, the billet is heated in a gas-fired furnace, induction heater, or electric furnace to the required forging temperature. Carbon steel billets are typically heated to 1,100°C–1,250°C. Alloy steel and stainless steel require specific temperature ranges based on their composition.
Heating must be uniform throughout the billet cross-section. Non-uniform heating causes uneven material flow during forging, leading to defects such as cold shuts, laps, and internal cracks.
Step 4 — Forging (Deformation)
The heated billet is placed in the forging die and deformed by the press, hammer, or roller. In closed die forging, the metal fills the die cavity under high pressure. In open die forging, the metal is progressively shaped through repeated hammer strokes and workpiece repositioning.
The forging operation may involve multiple hits or stages — a preform operation to rough-shape the billet, followed by a finish forging operation to produce the final geometry.
Step 5 — Trimming and Flash Removal
In closed die forging, excess metal that was squeezed out of the die cavity during forming (called flash) is trimmed using a trimming press or die. The trimmed flash is recycled as scrap.
In open die forging, the forged component may require rough machining to remove excess material and bring the component closer to its final dimensions.
Step 6 — Heat Treatment
Most forged components undergo post-forging heat treatment to achieve the required mechanical properties. Common heat treatment processes include:
- Normalizing — heating above the critical temperature and air cooling to refine grain structure and relieve internal stresses
- Quenching and tempering — rapid cooling (water or oil quench) followed by reheating to a lower temperature, producing high hardness and toughness
- Annealing — slow furnace cooling to soften the material for subsequent machining
- Stress relieving — low-temperature heating to reduce residual stresses without changing the microstructure
The specific heat treatment cycle is determined by the material grade and the mechanical property requirements of the application.
Step 7 — Finishing and Inspection
The final steps include surface cleaning (shot blasting or pickling), machining to final dimensions where required, and comprehensive quality inspection:
- Dimensional inspection against the engineering drawing
- Hardness testing (Brinell, Rockwell, or Vickers)
- Non-destructive testing — ultrasonic testing (UT) for internal soundness, magnetic particle inspection (MPI) for surface and near-surface defects, dye penetrant inspection (DPI) for surface cracks
- Microstructure examination — grain flow analysis, inclusion assessment
- Tensile testing — yield strength, ultimate tensile strength, elongation, reduction of area
- Impact testing — Charpy V-notch for toughness verification
Every forged component ships with a material test certificate (MTC) documenting chemical composition, mechanical properties, heat treatment records, and inspection results.
What counts as acceptable at this stage is set long before inspection. Forging tolerances vary by process and material, and the machining allowance follows from them.
Common Forging Defects
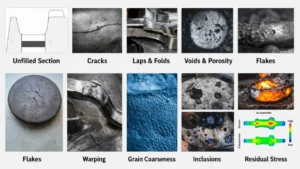
Despite being a highly controlled process, forging can produce defects if process parameters are not properly managed. Understanding these defects helps buyers evaluate supplier quality and specify appropriate inspection requirements.
Surface Defects
- Scale pits — shallow depressions on the surface caused by oxide scale not being fully removed before forging. Scale gets pressed into the surface during deformation.
- Laps and folds — overlapping metal on the surface caused by improper material flow during forging. The folded material does not fuse with the base metal, creating a surface discontinuity that acts as a stress raiser.
- Surface cracks — caused by excessive deformation, incorrect forging temperature, or material defects in the original billet.
Internal Defects
- Cold shuts — incomplete metal fusion where two material flow fronts meet but do not bond properly, usually caused by non-uniform heating or improper die design.
- Internal cracks — caused by forging at too low a temperature, excessive deformation speed, or forging a billet with pre-existing internal defects.
- Piping — a central void or cavity caused by shrinkage in the original ingot that was not fully closed during forging. An adequate reduction ratio (typically a minimum of 3:1) eliminates piping.
Dimensional Defects
- Die shift (mismatch) — misalignment between the upper and lower dies causing the top and bottom halves of the forging to be offset. Controlled by die locking mechanisms and regular die maintenance.
- Underfill — incomplete filling of the die cavity, caused by insufficient billet volume, incorrect heating, or inadequate forging force.
- Excess flash—more material squeezed out than expected, usually caused by oversized billets or worn die cavities.
Advantages of the Forging Process
Forging offers several distinct advantages over casting, machining from solid bar, and fabrication (welding):
- Superior strength — the grain structure is refined and aligned by the forging force, producing higher tensile strength, yield strength, and fatigue resistance than cast or machined components of the same material grade
- Grain flow orientation — the metal’s grain follows the contour of the forged shape, providing directional strength where the component needs it most
- Internal soundness — forging closes porosity, voids, and shrinkage cavities that may exist in the original billet or ingot, producing a fully dense component
- Consistency — closed die forging produces identical parts from the same die set, ensuring dimensional and metallurgical consistency across production batches
- Material efficiency — near-net-shape forging reduces material waste compared to machining from solid bar, where significant material is removed as chips
- Fatigue resistance — the continuous grain flow and absence of internal voids give forged components significantly better fatigue life than cast alternatives
- Impact toughness — forged components absorb energy without brittle fracture, making them preferred for safety-critical and high-load applications
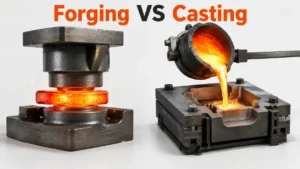
Forging vs Casting — Key Differences
| Factor | Forging | Casting |
| Process | Solid-state deformation under compressive force | Molten metal poured into a mold and solidified |
| Grain structure | Refined, aligned grain flow following part contour | Random, dendritic grain structure determined by solidification |
| Strength | Higher tensile, yield, and fatigue strength | Lower — limited by grain structure and potential internal defects |
| Internal soundness | Fully dense — porosity and voids eliminated by compression | May contain shrinkage, porosity, and gas cavities |
| Surface quality | Good — may require machining for final finish | Depends on casting method — sand casting rougher, investment casting smoother |
| Complexity | Limited to shapes achievable by die deformation | Excellent — complex internal passages, thin walls, intricate geometry possible |
| Tooling cost | High for closed die — dies are expensive | Lower for sand casting — higher for investment and die casting |
| Best application | High-strength, safety-critical, load-bearing components | Complex shapes, large housings, components where strength is not the primary concern |
The choice between forging and casting depends on the component’s mechanical requirements, geometry, production volume, and cost targets. Many industrial components use both processes — a cast housing with forged internal components or a forged blank with cast-on features.
At Sharma Technocast, our integrated manufacturing facility in Ahmedabad covers both forging and metal casting, allowing buyers to select the right process for each component — or combine both under a single supply chain.
The choice is rarely close once the loading is understood. We have set out how casting compares with forging in more detail, including where casting still wins on geometry and unit cost.
Materials Used in Forging
The forging process works with virtually all engineering metals and alloys. The most commonly forged materials in industrial applications include:
Carbon steel — AISI 1018, 1020, 1040, 1045, 1050. The workhorse of industrial forging. Used for shafts, flanges, fittings, structural components, and general engineering parts.
Alloy steel — AISI 4130, 4140, 4340, 8620. Alloyed with chromium, molybdenum, nickel, or vanadium for higher strength, hardenability, and wear resistance. Used for gears, crankshafts, connecting rods, and high-load structural components.
Stainless steel — 304, 316, 410, 17-4PH. Forged for corrosion-resistant applications in chemical processing, marine, food, pharmaceutical, and aerospace industries.
Tool steel — H13, D2, M2, S7. Forged for dies, molds, cutting tools, and high-wear industrial tooling.
Aluminum alloys — 2024, 6061, 7075. Forged for aerospace structural components, automotive suspension parts, and weight-sensitive applications.
Titanium alloys — Ti-6Al-4V. Forged for aerospace turbine components, medical implants, and high-performance applications requiring a high strength-to-weight ratio.
Copper alloys — Brass, bronze. Forged for electrical connectors, valve components, marine hardware, and corrosion-resistant fittings.
Forging Equipment
The primary equipment used in the forging process includes:
Forging hammers: deliver high-velocity impact blows to deform the workpiece. Types include drop hammers (gravity or power-assisted), counterblow hammers, and board hammers. Hammers are fast and suited for small to medium forgings.
Mechanical presses: use a crankshaft or eccentric mechanism to deliver a fixed-stroke pressing action. Mechanical presses provide consistent force and speed, suited for high-volume closed die forging of medium-sized components.
Hydraulic presses: use hydraulic cylinders to deliver controlled, high-force pressing at variable speed. Hydraulic presses are used for large open die forgings and precision press forging where slow, controlled deformation is required.
Screw presses: use a rotating flywheel and screw mechanism to deliver impact force. Screw presses combine the speed of hammers with the control of presses and are used for precision closed die forging.
Upsetters: horizontal forging machines designed specifically for upset forging operations such as bolt heads, fastener heads, and valve stems.
Ring rolling mills: specialized equipment for producing seamless forged rings from hollow preforms.
Industrial Applications of Forging
Forged components are used wherever strength, reliability, and long service life are non-negotiable:
- Automotive — crankshafts, connecting rods, steering knuckles, wheel hubs, transmission gears, axle shafts
- Aerospace — turbine discs, compressor blades, landing gear components, structural forgings, engine mounts
- Oil and gas — wellhead components, valve bodies, flanges, pipeline fittings, downhole tools, drill collars
- Power generation — turbine shafts, generator rotors, steam valve bodies, boiler fittings
- Mining and heavy equipment — track links, bucket teeth, crusher components, roller shafts
- Railway — wheel hubs, axles, couplings, brake components, rail fasteners
- Marine and shipbuilding — propeller shafts, rudder stocks, chain links, mooring components
- Defense — gun barrels, tank track components, ammunition casings, armored vehicle parts
- General industrial — hand tools, wrenches, spanners, hammers, clamps, jigs, and fixtures
Sharma Technocast supplies custom forged components to OEMs and industrial buyers across these sectors from our forging facility in Ahmedabad, India. For components that require post-forging precision machining to final dimensions, both operations are handled in-house under a single quality system.
How to Choose a Forging Manufacturer
When evaluating a forging manufacturer for your industrial components, consider the following:
- Process capability — does the manufacturer offer open die, closed die, roll forging, and upset forging, or only one method? A manufacturer with multiple forging methods can recommend the most appropriate process for your component.
- Material range — can they forge carbon steel, alloy steel, stainless steel, and specialty alloys, or are they limited to one material family?
- Size and weight range — what is the maximum billet weight and forged component size they can handle?
- In-house heat treatment — is post-forging heat treatment performed in-house with documented time-temperature records, or outsourced to a third party?
- Machining capability — can they machine forged blanks to final dimensions in-house, eliminating the need for a separate machining vendor?
- Quality and certification — are they ISO 9001 or AS9100 certified? Do they provide full MTC, NDT reports, and dimensional inspection documentation?
- Integrated services — a manufacturer that also offers casting, machining, and fabrication under one roof simplifies your supply chain and reduces coordination overhead.
There is more to it than press capacity. Our guide to choosing a forging manufacturer covers the questions worth asking at RFQ stage, from material traceability through to lead time consistency.
Frequently Asked Questions
Q1. What is the forging process?
The forging process is a solid-state metal forming operation that shapes metal using compressive force — applied through hammering, pressing, or rolling — to produce components with refined grain structure, superior strength, and improved mechanical properties compared to cast or machined alternatives.
Q2. What are the main types of forging?
The main types are open die forging, closed die forging, roll forging, upset forging, and ring rolling. These are further classified by temperature into hot forging, warm forging, and cold forging.
Q3. What is the difference between open die and closed die forging?
Open die forging uses flat or simple dies that do not fully enclose the workpiece, allowing metal to flow laterally. It is used for large, heavy components. Closed die forging uses shaped dies that contain the full impression of the part, producing tighter tolerances and better surface finish. It is used for medium to high-volume production.
Q4. What is the difference between hot forging and cold forging?
Hot forging heats the metal above its recrystallization temperature (typically 950°C–1,250°C for steel), allowing easier deformation and complex shapes. Cold forging deforms metal at room temperature, producing better surface finish and tighter tolerances but requiring higher forming force and limiting part size.
Q6. What are the advantages of forging over casting?
Forging produces components with higher strength, better fatigue resistance, continuous grain flow, and no internal porosity or shrinkage cavities. Casting is preferred for complex shapes and large thin-walled components where strength is not the primary requirement.
Q7. What are common forging defects?
Common defects include surface laps, cold shuts, scale pits, internal cracks, die shift (mismatch), underfill, and piping. These are controlled through proper heating, die design, material quality, and process parameter management.
Q8. What materials can be forged?
Most engineering metals can be forged including carbon steel, alloy steel, stainless steel, aluminum, titanium, copper, and brass. The material selection depends on the application’s strength, temperature, corrosion, and weight requirements.
Q9. What industries use forged components?
Forging is used across automotive, aerospace, oil and gas, power generation, mining, railway, marine, defense, and general industrial applications wherever high-strength, reliable components are required.
Q10. How is forging quality verified?
Forging quality is verified through dimensional inspection, hardness testing, non-destructive testing (UT, MPI, DPI), tensile testing, impact testing, grain flow analysis, and documented material test certificates.
Q11. What is grain flow in forging?
Grain flow is the alignment of the metal’s internal crystal structure along the contour of the forged part. Proper grain flow increases strength, fatigue life, and impact resistance in the direction of maximum stress. Grain flow is unique to forging — casting and machining do not produce directional grain alignment.
Q12. How do I choose the right forging manufacturer for my project?
Select a forging manufacturer based on their experience, forging capabilities, material expertise, quality certifications, machining facilities, inspection processes, and ability to produce components according to your drawings and specifications. A supplier that offers forging, CNC machining, heat treatment, and quality testing under one roof can improve consistency, reduce lead times, and simplify your supply chain.