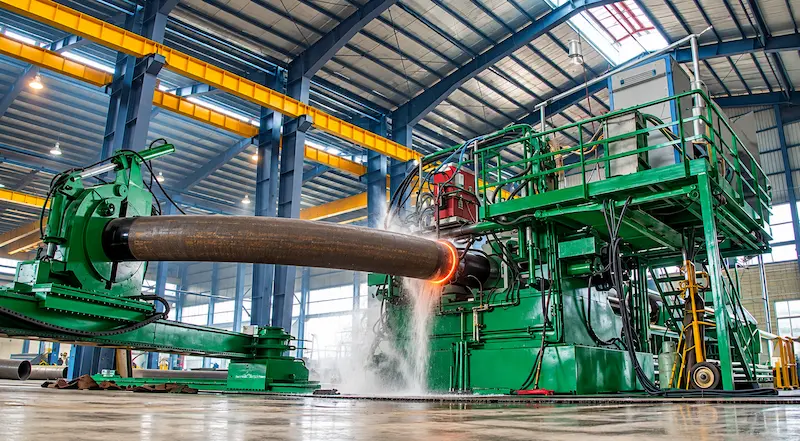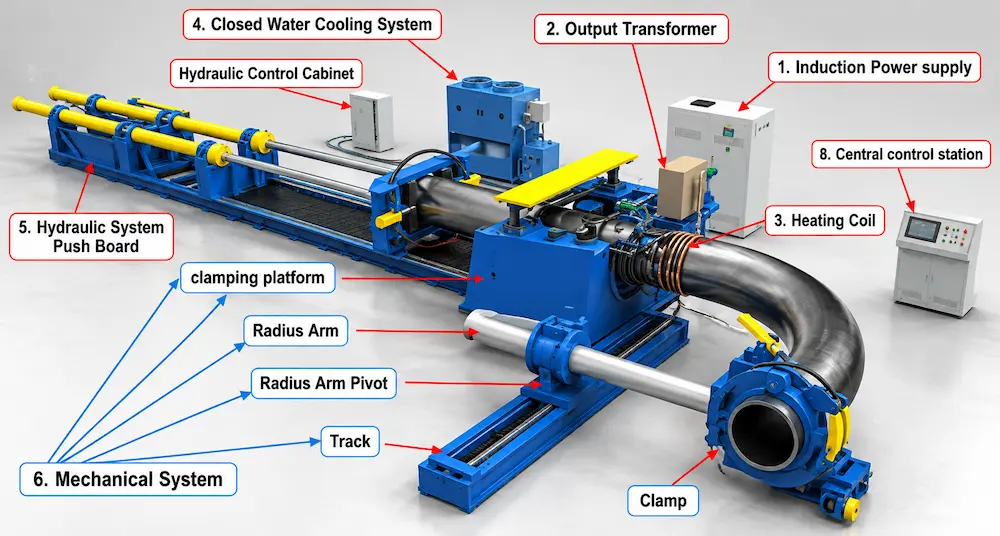
Two standard machines for 76 mm up to 48″ pipe, plus custom machines built to your specification.
| Specification | STC 325D-14T | 48″ machine (STC PB-1219) |
|---|---|---|
| Pipe outside diameter | 76–325 mm | 324–1219 mm (12″–48″) |
| Wall thickness | Up to 25 mm | 6–20 mm |
| Materials | MS, stainless steel, titanium | API 5L up to Grade X70; carbon, alloy and stainless steel |
| Bending radius | 1.5D–3D | 2D, 2.5D, 3D, 4D, 5D |
| Bending angle | On request | 20°–180° |
| Maximum pipe length | 12 m | 12 m |
| Induction heating | 600 KVA, 500–1000 Hz | 1000 kW IGBT, 0.8–1.2 kHz |
| Pushing force | 85 MT | 195 T |
| Hydraulic pressure | 21 MPa | 20 MPa |
| Water cooling | 6 cooling coils | Closed water cooling system |
Need a different pipe size, radius or material? Send your specification and we will propose a machine within 24–48 hours.
Get Machine Price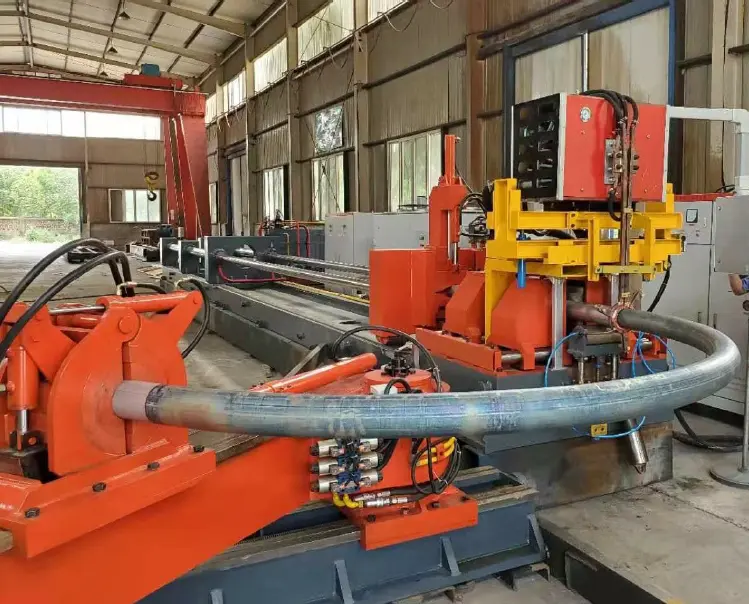
The STC 325D-14T is our induction pipe bending machine for small and medium-diameter, heavy-wall pipe: outside diameters from 76 to 325 mm with walls up to 25 mm, in mild steel, stainless steel and titanium. A 600 KVA induction heating system working at 500–1000 Hz heats a narrow band of the pipe, an 85 MT hydraulic push at 21 MPa moves it through the bend, and water cooling coils fix the shape, giving tight 1.5D to 3D bends on pipes up to 12 m long.
| Model | STC 325D-14T |
|---|---|
| Pipe outside diameter | 76–325 mm |
| Maximum wall thickness | Up to 25 mm |
| Materials | Mild steel, stainless steel, titanium |
| Bending radius | 1.5D–3D |
| Maximum pipe length | 12 m |
| Induction heating power | 600 KVA |
| Frequency | 500–1000 Hz |
| Hydraulic operating pressure | 21 MPa |
| Maximum pushing force | 85 MT |
| Water cooling coils | 6 |
For pipeline and plant projects, we design and build a large-diameter induction pipe bending machine that bends line pipe from 12″ to 48″ (324–1219 mm OD) with walls from 6 to 20 mm, in API 5L up to Grade X70, carbon steel, alloy steel and stainless steel. It makes elbows and U-bends at 2D to 5D radius, from 20° to 180°, on pipes up to 12 m long. The machine also bends square and rectangular hollow sections and I/H beams.
| Pipe outside diameter | 12″–48″: 324, 406, 457, 508, 560, 610, 668, 764, 864, 914, 1016, 1219 mm |
|---|---|
| Wall thickness | 6–20 mm |
| Maximum pipe length | 12 m |
| Bending radius | 2D, 2.5D, 3D, 4D, 5D |
| Bending angle | 20°–180° |
| Bend types | Elbows and U-bends |
| Materials | API 5L up to X70, carbon steel, alloy steel, stainless steel; seamless and welded pipe |
| Other sections | Square and rectangular hollow sections, I/H beams |
| Bending speed | 0–100 mm/min, adjustable |
|---|---|
| Radius tolerance | ≤ 1% of OD |
| Angle tolerance | ± 0.5° |
| Ovality | 1–6% |
| Wall thinning | ≤ 15% at 2.5D; ≤ 8% at 4D and above |
| Heating temperature | Up to 1100 °C, controlled to ± 15 °C |
|---|---|
| Temperature control | 2 infrared pyrometers with closed-loop PID control |
| Power supply | 1000 kW IGBT, LC series resonant, modular design with film capacitors |
| Frequency | 0.8–1.2 kHz |
| Duty cycle and efficiency | 100% duty, about 90% efficiency |
| Output transformer | 10,000 kVA, water-cooled |
| Coils | Induction coil and spray-cooling ring set for each pipe size, with electric 2-axis centring |
| Push cylinders | 2 cylinders, bore 250 mm, rod 299 mm OD, stroke 10,000 mm |
|---|---|
| Pushing force | 195 T at 20 MPa |
| Hydraulic drive | Servo / VFD controlled, 150 L/min |
| Clamping and dies | 2 clamps and 10 dies |
| Bending arm | Servo-controlled pivot arm |
| Cooling | Closed-loop stainless steel water cooling system |
| Controller | PLC with 10″ touch panel and SCADA |
|---|---|
| Recipes | Stored bending programs for each pipe size and radius |
| Monitoring | Live temperature, speed and pressure, with alarms |
| Data | Bend records exported by USB |
| Machine weight | About 200 T |
|---|---|
| Floor area | 31 m × 18 m |
| Clear height | 6 m or more |
| Cranes | 2 overhead cranes, 10 t or more |
| Power | About 1300 kVA, 3-phase 380 V, 50 Hz |
The pipe is checked for diameter, wall thickness and material grade, marked for the bend, and loaded onto the machine bed.
The clamps, bending arm and induction coil are set for the required bending radius and angle, and the bending program is loaded on the PLC.
An induction coil heats a narrow ring of the pipe to bending temperature, while the rest of the pipe stays cold and holds its shape.
The hydraulic cylinders push the pipe slowly through the coil while the arm turns, so only the heated ring bends to the set radius.
A water spray just after the coil cools the bent section at once, which fixes the radius and limits ovality and wall thinning.
The finished bend is checked for radius, angle, ovality and wall thickness against the drawing.
Long-radius bends and elbows for cross-country oil and gas pipelines in API 5L line pipe.
Bends for steam, feed-water and cooling-water piping in thermal and power plants.
Process piping bends in carbon steel, alloy steel and stainless steel for refineries and petrochemical units.
Smooth, one-piece bends that cut the number of welded joints in chemical plant piping.
Large-diameter bends for water supply mains and pumping stations.
Bending of heavy-wall pipe, hollow sections and beams for structures and shipbuilding, alongside our steel fabrication work.
The supplied machine information identifies Oil & Gas, Power & Energy, Petrochemical, Chemical Processing, Water Transmission and Heavy Engineering among the relevant applications.