

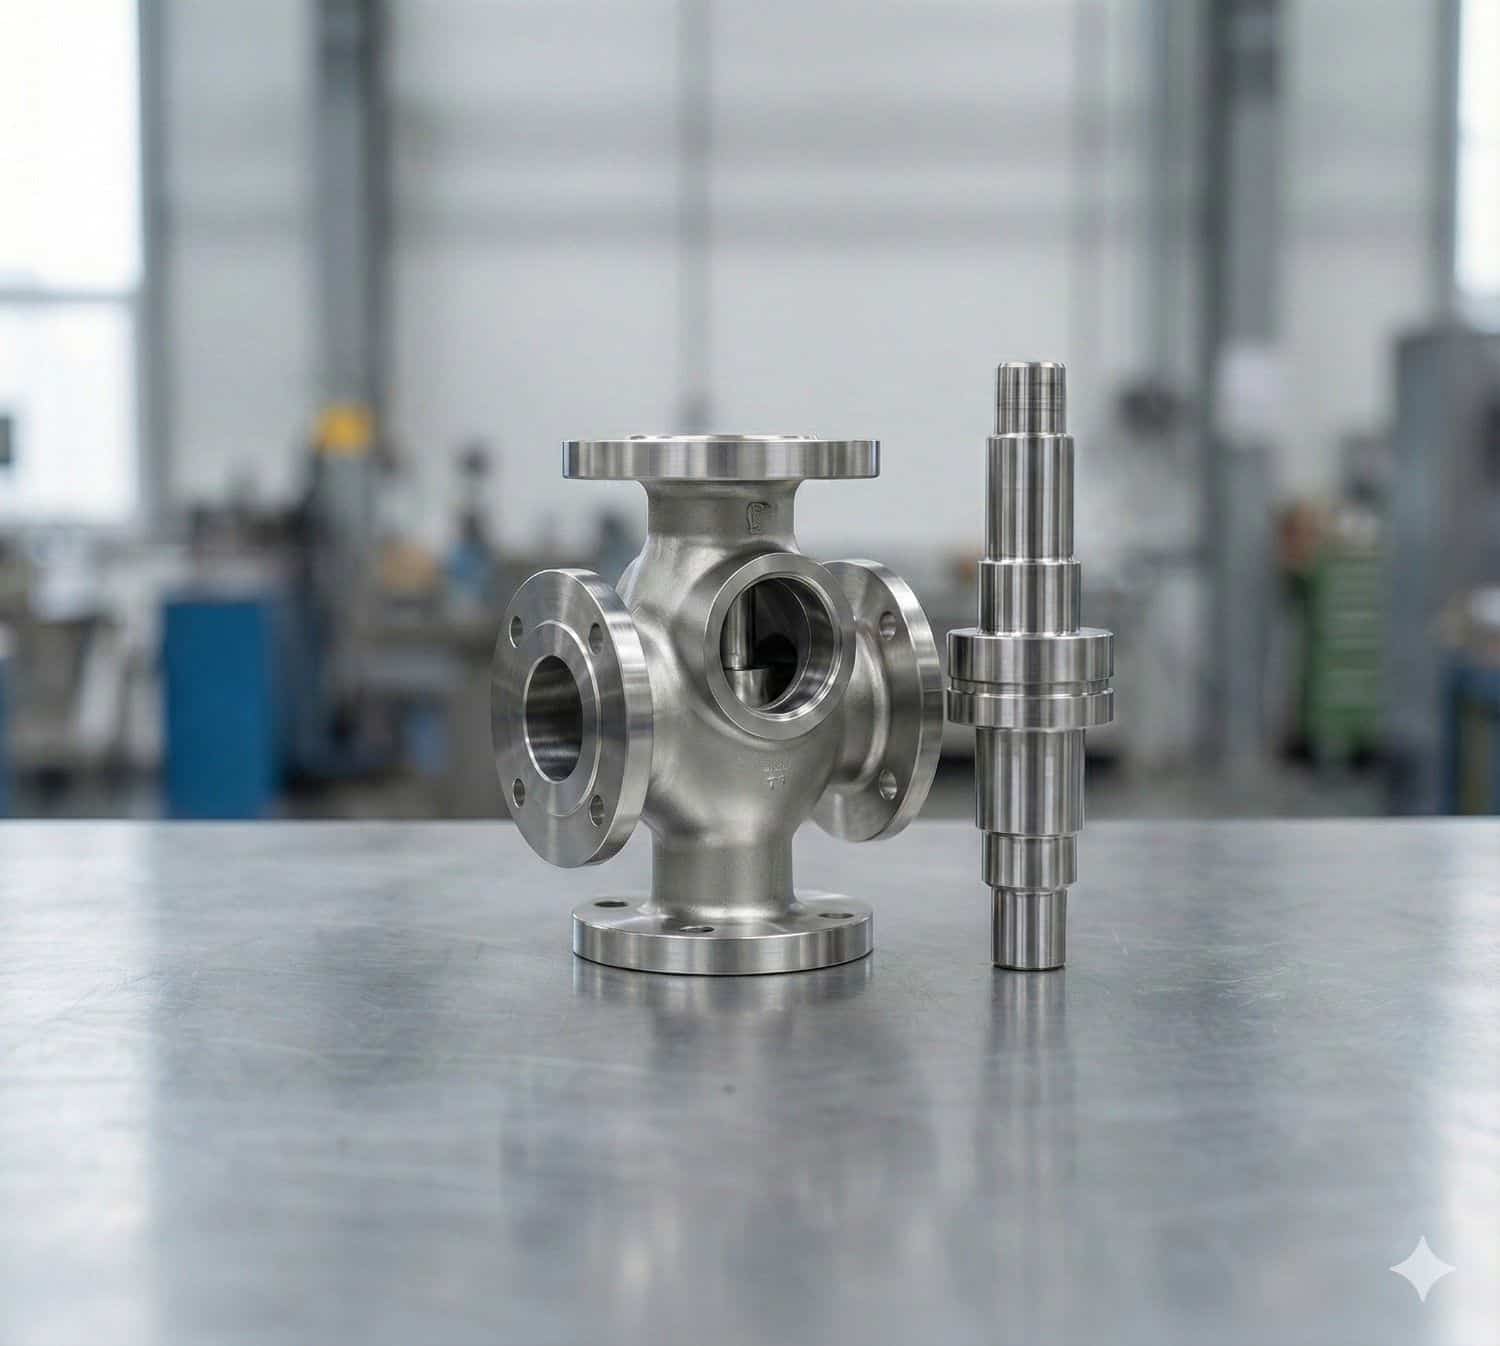
Eight casting routes under one roof, from 10 g die castings to 800 kg centrifugal castings, all machined, heat-treated and inspected in-house.
| Process | Max size | Part weight | Tolerance / wall | Best for |
|---|---|---|---|---|
| Sand casting (flask) | 650 × 550 × 200 mm | 1.5 – 25 kg | Machined to drawing | Housings, brackets, pump parts |
| Sand casting (flaskless) | 750 × 650 × 250 mm | 10 – 60 kg | Machined to drawing | Medium-volume industrial parts |
| Sand casting (no-bake) | 1000 × 1100 × 350 mm | 10 – 200 kg | Machined to drawing | Large, complex heavy parts |
| Investment casting | As per drawing | 0.3 – 99 kg | ±0.1 mm, min. wall 3 mm | Valves, aerospace, precision parts |
| Centrifugal casting (horizontal) | OD 550 mm, ID 75 mm | 50 – 800 kg | Machined to drawing | Sleeves, bushes, liners, rings |
| Pressure die casting (aluminium) | 400 × 400 × 150 mm | 10 g – 5 kg | Thin walls, high repeatability | Housings, covers, brackets, heat sinks |
| Zinc die casting (hot chamber) | On request | On request | Very thin walls, fine detail | Fittings, hardware, connectors |
| Gravity die casting (aluminium) | As per drawing | Up to 15 kg | Dense, good surface finish | Heavier housings, pump & valve bodies |
Need a size or alloy outside these ranges? Send your drawing and we will confirm feasibility within 24–48 hours.
Send Your RFQWe operate a fully Integrated Metal Casting Manufacturing Facility in India equipped to handle casting and machining of graded cast iron, aluminum, brass, bronze, and stainless steel materials.
This integrated workflow ensures faster turnaround, higher quality control, and optimized cost efficiency, making Sharma Technocast one of the most reliable metal casting companies in India.
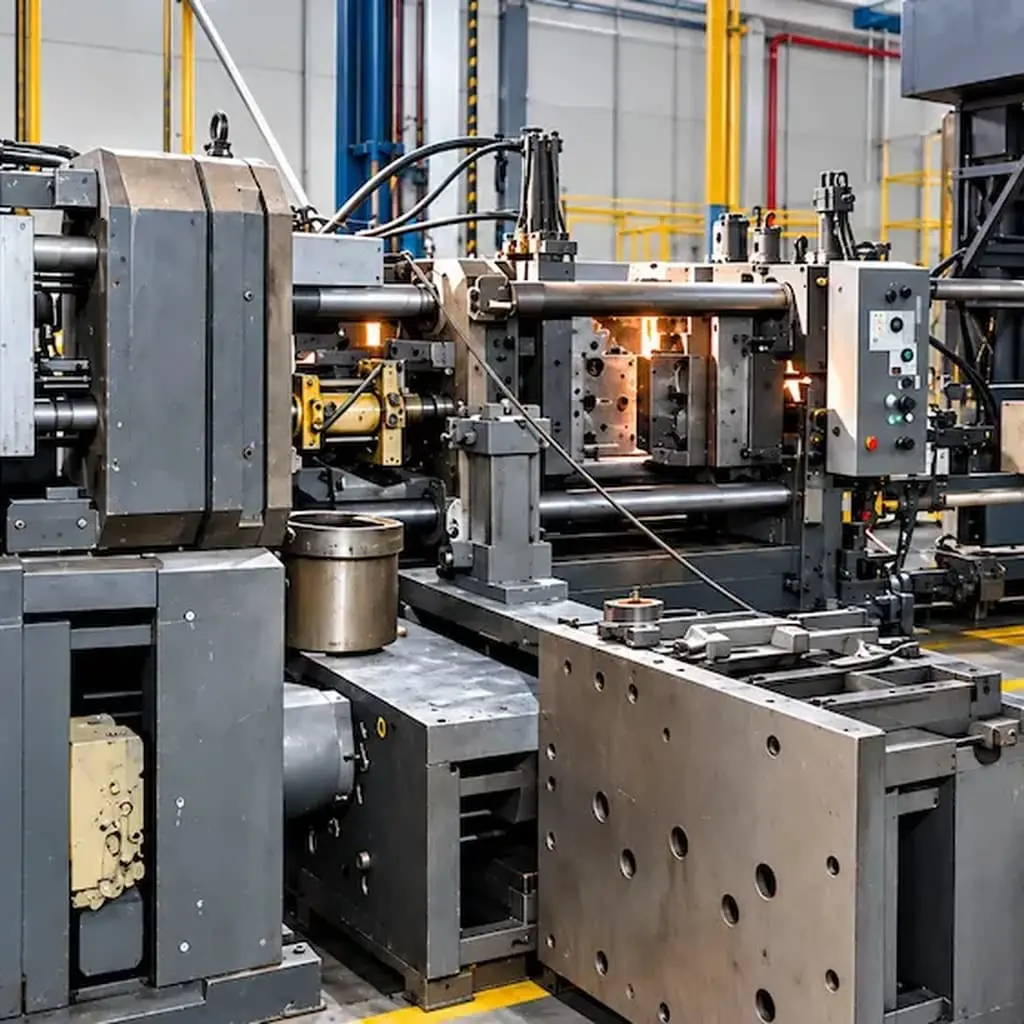
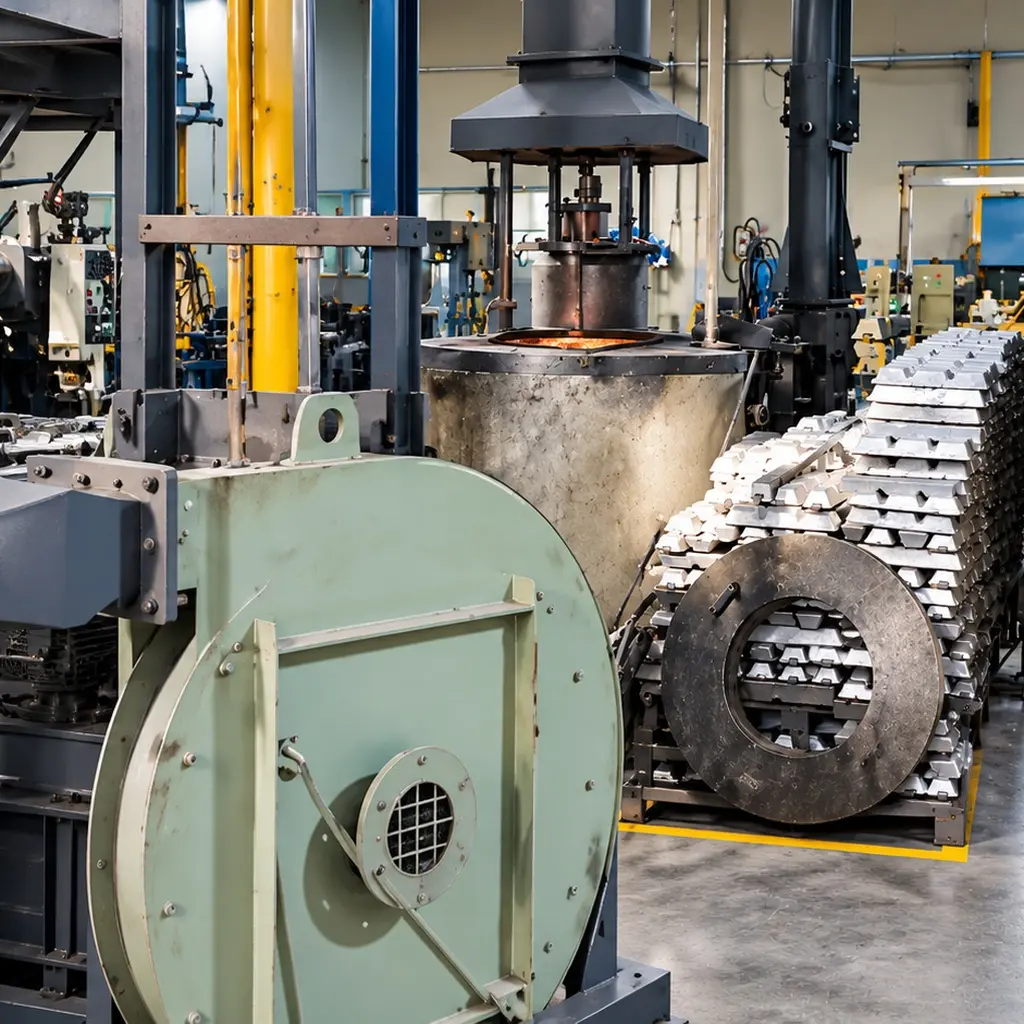
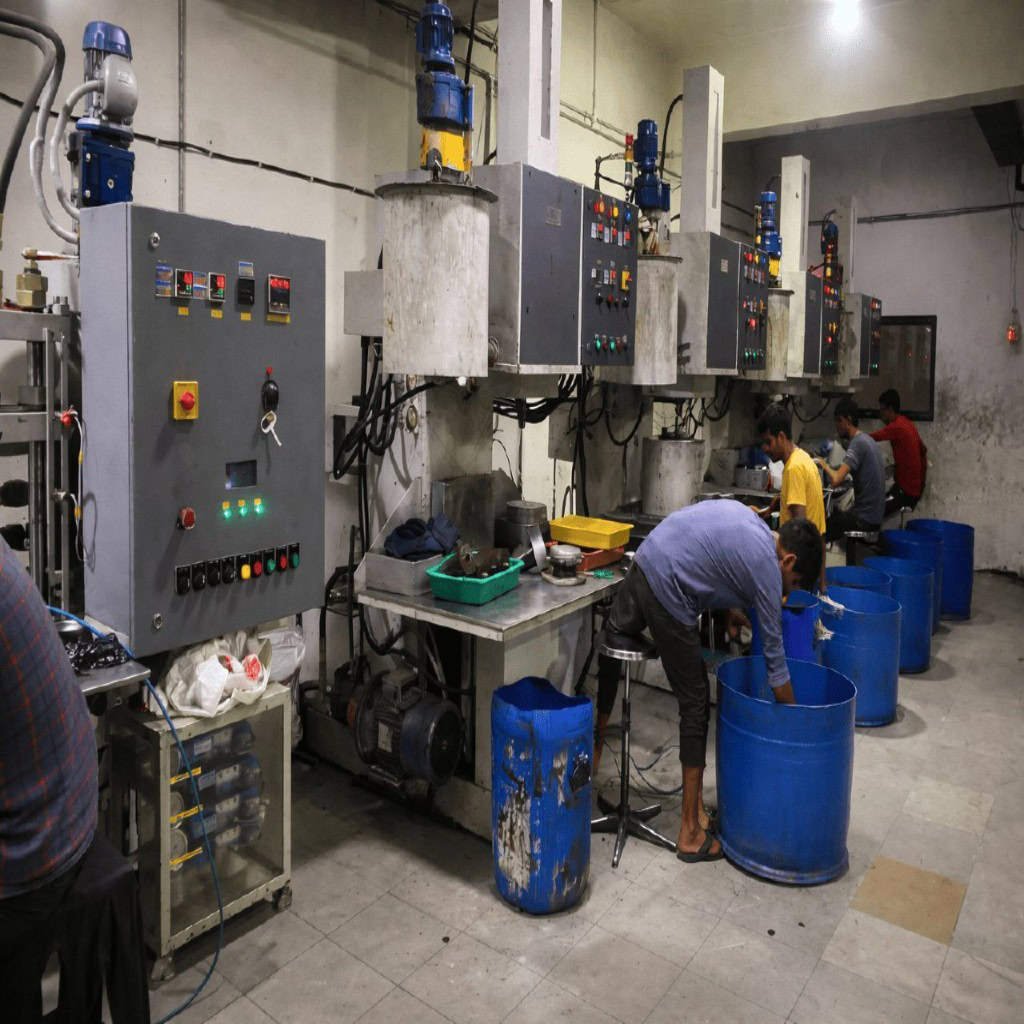
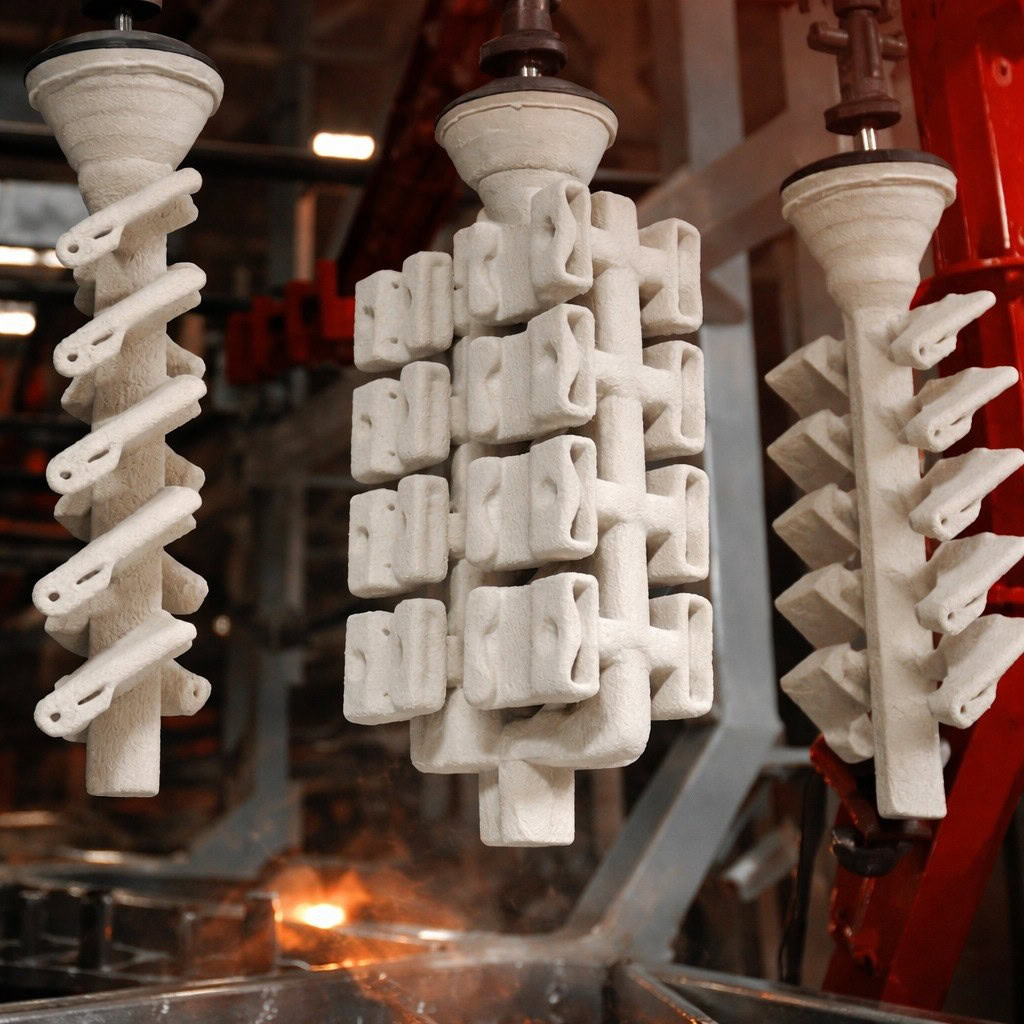
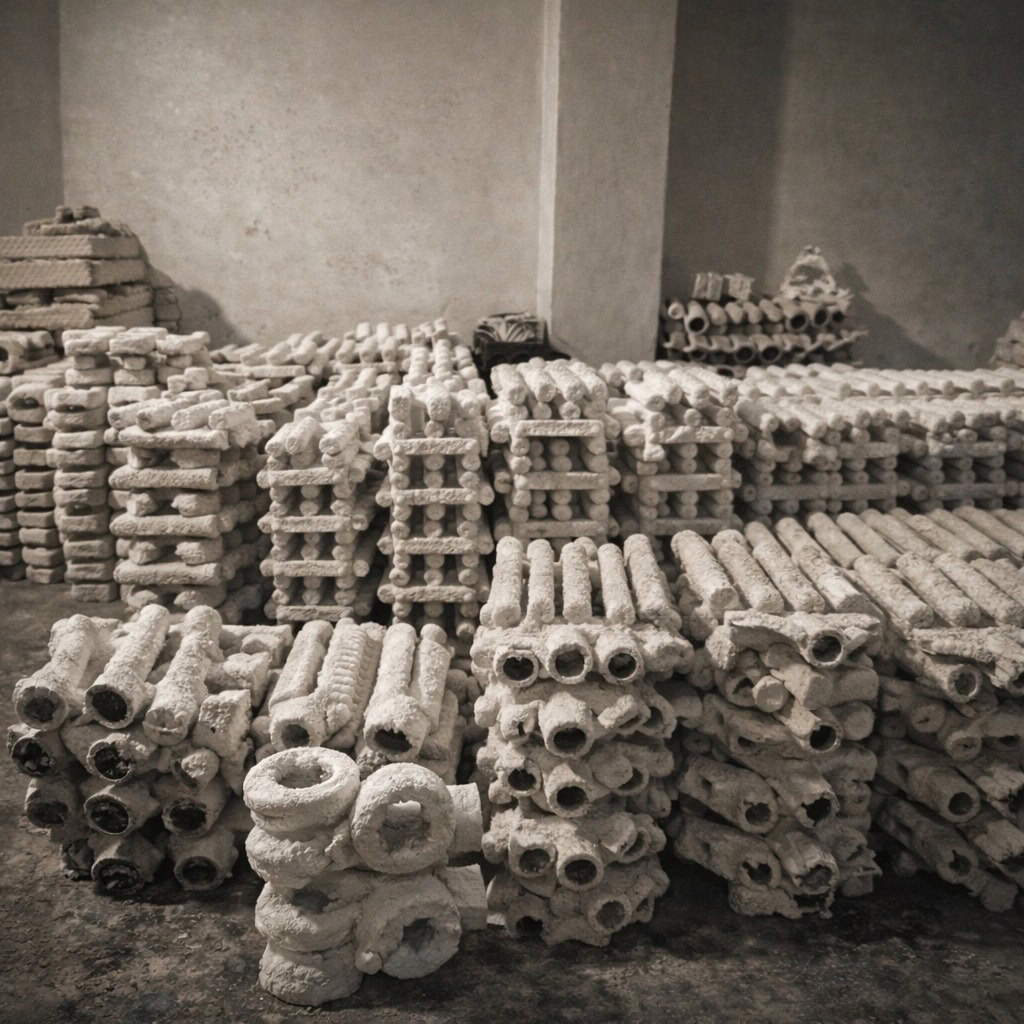
From a rough concept sketch to a detailed 3D CAD model, we manage your project from design to delivery. With lead times between 4 to 17 weeks, our engineering team offers:
Design consultation and prototyping
Casting simulation and material selection
Production planning and delivery management
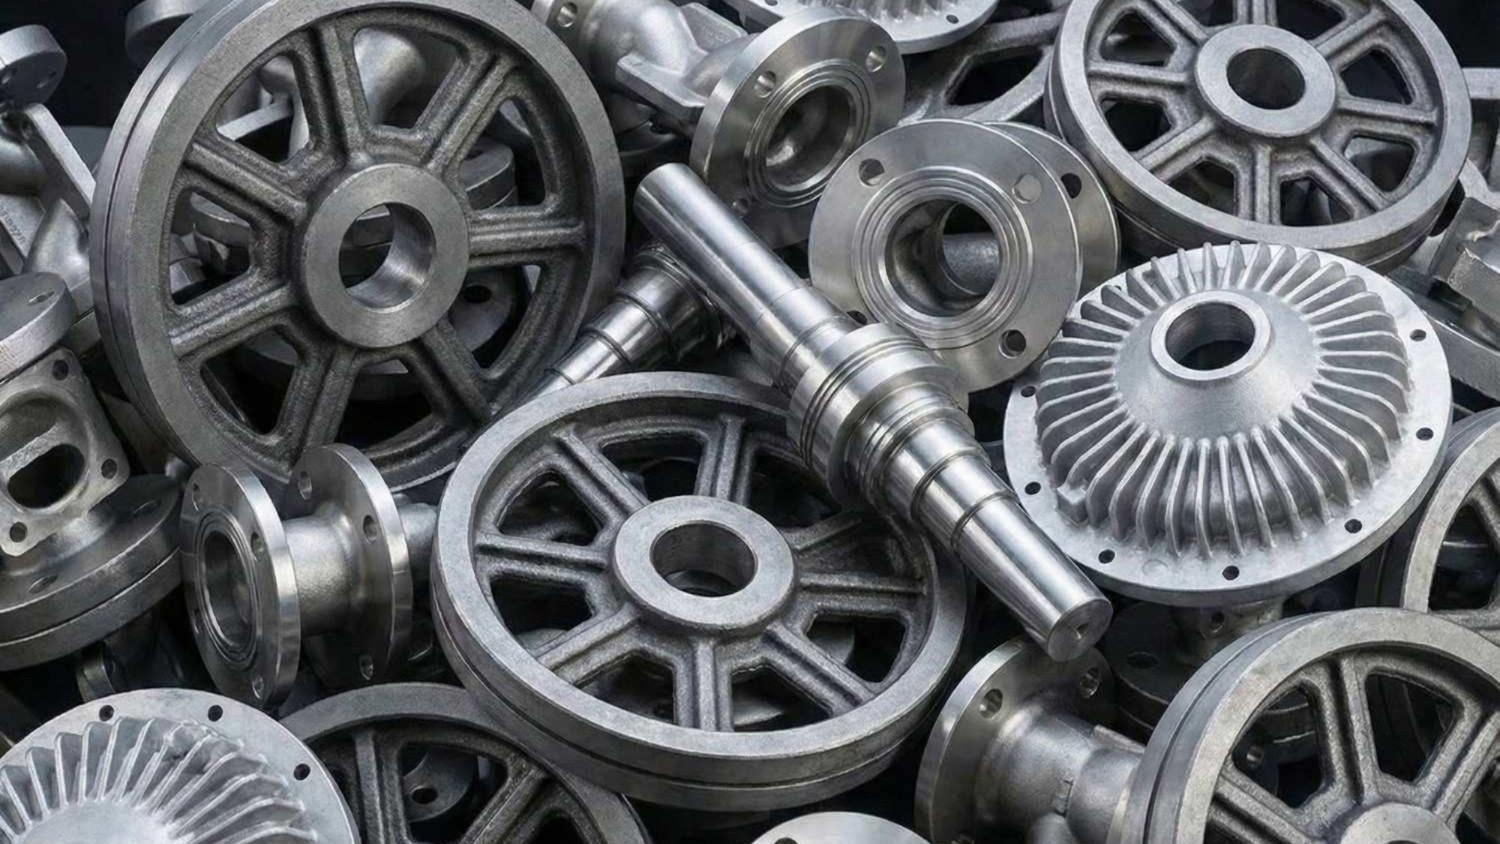
Our commitment is simple — precision, reliability, and performance at every stage
If you are still working out which route suits your component, our guide to how the metal casting process works sets out each method and where it fits.
Integrated Casting Lines for Sand Casting, Investment Casting, and Centrifugal Casting
Our sand casting facility is engineered to deliver robust, cost-effective castings for medium to large components with complex geometries. With flexible moulding methods and high pouring capacity, we support heavy engineering, oil & gas, automotive, and infrastructure applications.
From prototype development to bulk production, our sand casting process ensures dimensional accuracy, structural integrity, and consistent quality.
We have covered the sand casting process in detail separately, including mould preparation and the point where the method reaches its size and finish limits.
Maximum Part Size
| L | 650 mm / 26 in |
| B | 550 mm / 22 in |
| W | 200 mm / 8 in |
| Min | 1.5 kg / 3 lbs |
| Max | 25 kg / 55 lbs |
Maximum Part Size
| L | 750 mm / 30 in |
| B | 650 mm / 26 in |
| W | 250 mm / 10 in |
| Min | 10 kg / 22 lbs |
| Max | 60 kg / 132 lbs |
Maximum Part Size
| L | 1000 mm / 39 in |
| B | 1100 mm / 43 in |
| W | 350 mm / 14 in |
| Min | 10 kg / 22 lbs |
| Max | 200 kg / 441 lbs |
Our investment casting process is ideal for high-precision, near-net-shape components requiring excellent surface finish and tight tolerances. This method significantly reduces machining requirements and is widely used for aerospace, defense, valve, pump, and precision engineering parts.
We support complex profiles, thin walls, and intricate internal features with repeatable accuracy.
Our guide walks through the investment casting process step by step, covering how the wax pattern is built and how the ceramic shell forms around it.
| Typical Part Weight Range | 0.3 kg – 99 kg |
| Part thickness | 3 mm / 0.11 in |
| Accuracy | 0.1 mm |
Stainless Steel: Grades like 304, 316, and 17-4PH offer excellent corrosion resistance and strength for medical, food, and marine parts. Aluminum Alloys: Lightweight, corrosion-resistant, used in aerospace and electronics, often with copper, magnesium, or silicon additions. Carbon & Alloy Steels: Provide structural integrity, used in motors, valves, and firearms. Copper Alloys: Includes brass and bronze for electrical and general industrial uses. Nickel & Cobalt Alloys: High-performance superalloys for extreme temperature and creep resistance (e.g., turbine components). Titanium Alloys: Valued for high strength-to-weight ratio in aerospace.
Centrifugal casting spins the mould at high speed while molten metal is poured, forcing the metal outward against the mould wall. The result is a dense, fine-grained wall with very low porosity, ideal for round parts such as sleeves, bushes, liners, rings and pipe sections. We cast horizontally for long cylindrical parts (up to 550 mm OD and 800 kg) and vertically for short rings and flanges (up to 600 mm OD), then machine them to final size in-house.
For rings and flanges up to 600 mm OD. Sizes on request.
Die casting forces molten aluminium or zinc into a hardened steel die, producing parts with excellent dimensional repeatability, thin walls and a smooth as-cast finish. Because the die is reused thousands of times, it is the most economical process for medium to high volumes. We run cold-chamber pressure die casting machines from 120 to 350 tonnes for aluminium, a hot-chamber machine for zinc, and gravity die casting for heavier parts, all backed by in-house CNC machining, finishing, and inspection.
Aluminium and zinc die castings from 10 g to 15 kg, machined, finished, and inspected in-house for medium to high volumes.
Aluminium Pressure Die Casting |
Zinc Die Casting |
Gravity Die Casting |
|
| Process | High-pressure injection into a steel die for thin-walled, complex aluminium parts. | Hot-chamber casting of Zamak for small, highly detailed parts ready for plating. | Aluminium poured into a permanent steel mould for denser, heavier parts. |
| Machines | 350 T ×1, 180 T ×2, 120 T ×2 (cold chamber) | Hot chamber | Permanent steel moulds |
| Part weight | 10 g – 5 kg | On request | Up to 15 kg |
| Max part size | 400 × 400 × 150 mm | On request | As per drawing |
| Alloys | ADC12, A380 | Zamak 3, Zamak 5 | Aluminium alloys |
| Capacity | ~100 tonnes / month | On request | On request |
| Best for | Housings, covers, brackets, heat sinks | Fittings, locks, hardware, connectors | Heavier housings, pump & valve bodies |
Typical die cast parts: pump and motor housings, gearbox covers, valve bodies, brackets, heat sinks, electrical enclosures, locks, fittings and automotive components.
Automatic PLC-based Sand Plant with molding
track line system
CNC, VMC, VTL, and HMC machining centers
ARPA Moulding Machines and No-bake Molding setups
Dust collectors, sand coolers, and 75-ton sand storage
Fully equipped testing laboratory
This world-class infrastructure allows us to maintain precision, repeatability, and reliability across all production batches.
Automated PLC-controlled processes for consistent quality
Ferrous and non-ferrous casting capabilities
Rapid RFQ responses and short tooling lead times (as low as 2 weeks)
No minimum order quantity — perfect for both prototypes & production
Full traceability with test certificates for chemical & mechanical properties
Competitive pricing and global shipping capability
Each material is chosen for its mechanical strength, corrosion resistance, and heat performance, tailored for sectors like automotive, energy, oil & gas, and heavy engineering.
Sharma Technocast is ISO 9001:2015 certified (accredited and verifiable on IAF CertSearch). Every casting is traceable to its heat, and test certificates are supplied with each shipment.
| Certification | ISO 9001:2015 Quality Management System |
|---|---|
| In-house testing | Chemical analysis, hardness testing, dimensional inspection |
| NDT on request | X-ray (radiography) and ultrasonic testing |
| Documents supplied | Material test certificates, dimensional inspection reports, NDT reports where specified |
| Traceability | Every casting traceable to its heat number |
Precision meets craftsmanship.
Our machining division performs turning, milling, drilling, threading, and surface finishing with exact tolerances. Using modern CNC and VMC systems, every part achieves dimensional precision and flawless functionality — ready for assembly or direct application.
To ensure your parts perform and look their best, we offer:
Quality is at the core of Sharma Technocast.
Every casting undergoes multi-stage testing using:
Our in-house assembly division integrates castings, machined components, and subassemblies into ready-to-use engineered solutions. Whether it’s a small component or a complex industrial product, we ensure precision fit, functionality, and reliability — saving clients time and resources.
What size and weight of castings can you produce?
Investment castings range from 0.3 kg to 99 kg with walls down to 3 mm. Sand castings go up to 1000 x 1100 x 350 mm and 200 kg using the no-bake process. Horizontal centrifugal castings reach 550 mm outside diameter and 800 kg, and vertical centrifugal castings up to 600 mm outside diameter. Aluminium pressure die castings range from 10 grams to 5 kg, and gravity die castings go up to 15 kg.
Send your drawing (PDF, STEP or IGES), material grade, quantity, required standard and target delivery date through our RFQ form or to [email protected]. We usually reply with a quotation within 24–48 hours.